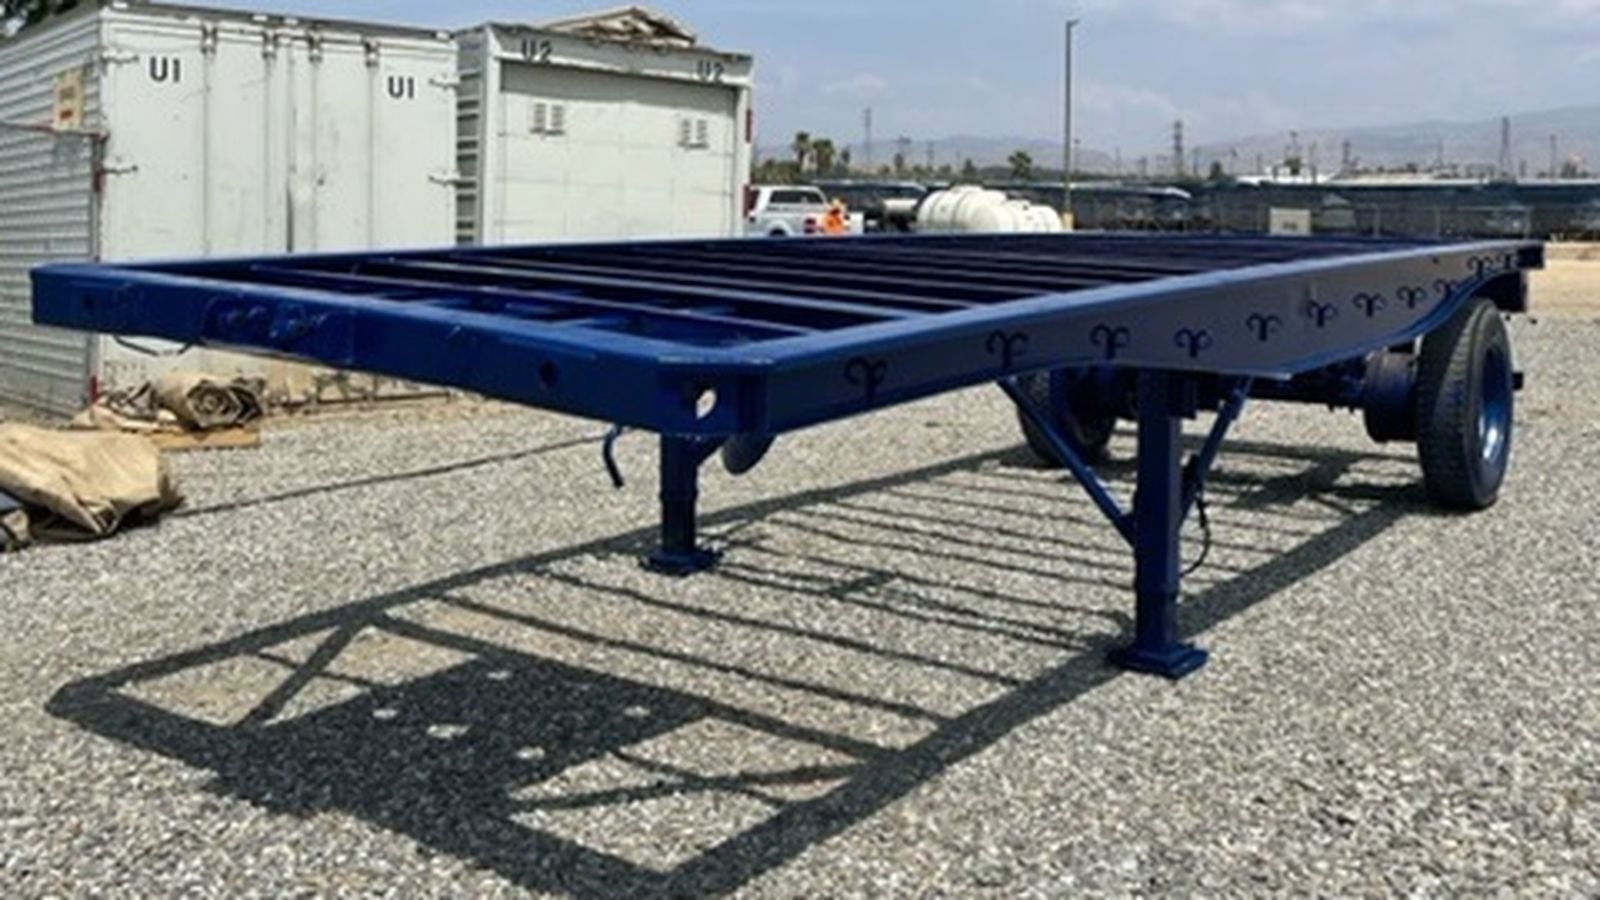
OEM shops need fast throughput and coatings that last in the field. How to pick a coating system that fits your production line and your customer's environment.
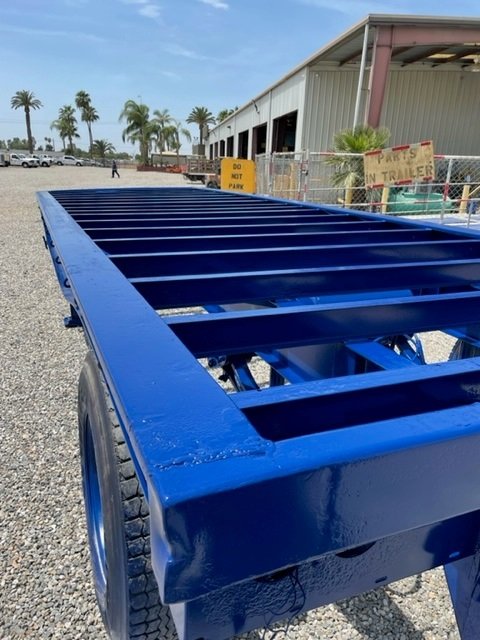
The right OEM coating system keeps the production line moving and still protects equipment in the environment where the customer will run it.
For OEM engineering and manufacturing managers, and for the engineers and owners who write equipment specifications, the coating decision balances line speed against field durability. Those goals only conflict when the system is chosen for the paint line first and the end-use environment second.
This article covers how to define the field exposure, which shop factors control throughput, where surface preparation decides durability and how to compare systems on cost per unit shipped.
What Is an OEM Coating System?
An OEM coating system is the set of primer, intermediate and finish coats applied in the manufacturer's shop before equipment ships. It has to fit the production schedule and still protect the equipment once it is installed, often far from the plant and in conditions the shop never sees.
The best-fitting system is usually the one with the fewest steps and the shortest handling time that still meets the end-use environment. Getting there requires defining that environment first.
Field Environment: The Starting Point for Selection
Equipment built in one plant may end up on a rooftop, a coastal dock, a wastewater plant or a chemical facility. The coating has to be selected for the worst realistic exposure, not the average one.
The international standard for protective paint systems on steel (ISO 12944-2) gives a useful vocabulary. It classifies atmospheric environments into corrosivity categories from C1 (very low) through C5 (very high) and CX (extreme), with separate categories for immersion and buried service.
Many end-user specifications now reference ISO 12944 or call out laboratory test hours, so knowing the expected category early prevents a mismatch later. Beyond corrosivity, OEM teams should define the following:
- Ultraviolet Exposure: Whether the customer expects color and gloss to hold for branding.
- Chemical Contact: Splash, fumes or washdown chemicals in service.
- Mechanical Damage: Abrasion, impact and handling during shipping and installation.
- Service Temperature: Including hot surfaces on process equipment.
- Wet Areas: Sumps, trays and lower panels that see immersion or frequent wetting.
Throughput: Cure, Handling and Recoat
On a production line, the coating's schedule is the line's schedule. The properties that matter most are listed below, and each should be read at the temperature and humidity the shop actually runs:
- Time to Handle: When parts can be moved without marking the film.
- Time to Stack or Pack: When parts can touch without blocking or sticking.
- Recoat Window: The minimum and maximum time between coats.
- Pot Life: How long mixed material remains usable.
Reducing the number of coats is the most direct way to increase throughput. Direct-to-metal and high-build single-coat finishes can replace a primer and finish in moderate exposures, while more corrosive categories generally need a zinc-rich or epoxy primer under a UV-stable finish.
The honest tradeoff is that fewer coats leave less margin for thin spots, edges and handling damage. Fast-recoat primers can shorten the time between coats without removing a layer of protection.
Force curing with heat can increase line speed, but only within the temperature range the product allows. Curing too hot or too fast can trap solvent or cause defects, so any accelerated cure schedule should be confirmed with the manufacturer before it is built into the line.
Surface Preparation: Where Shop Durability Is Won
Shop conditions offer advantages the field rarely has: controlled blasting, consistent abrasive and good lighting. That advantage is lost if preparation is rushed to keep the line moving.
Key preparation requirements for OEM steel include:
- Blast Cleaning: Near-white metal blast cleaning (SSPC-SP 10/NACE No. 2) or commercial blast cleaning (SSPC-SP 6/NACE No. 3), as the system requires.
- Surface Profile: Measured with replica tape or depth gauges (ASTM D4417) and matched to the primer's requirement.
- Soluble Salts: Tested where parts may have been exposed to deicing salts or coastal storage.
- Edges and Welds: Sharp edges, weld spatter and laser- or plasma-cut edges are prepared to the grades described for welds, edges and imperfections (ISO 8501-3), because they are where shop coatings fail first.
- Contaminants: Oil, coolant and drawing compounds are removed by solvent cleaning (SSPC-SP 1) before blasting.
The HPC article The Importance of Surface Preparation with High Performance Coatings covers the reasoning in more depth. For corrosive categories, Unlocking the Power of Zinc Primers in High Performance Coating Systems explains when a zinc-rich primer earns its place.
Cost Per Unit Shipped: Beyond the Price per Gallon
The lowest material price rarely produces the lowest cost per unit. Across OEM operations, the larger cost drivers typically include:
- Line Time: Labor and booth time for each additional coat.
- Rework: Runs, dry spray, low film build or blocking damage.
- Field Touch-Up: Repairs after shipping and installation.
- Warranty Exposure: Claims and strained customer relationships when equipment rusts or fades early.
- Brand Consistency: Color matching across production runs when the equipment carries the company's name.
A system that costs more per gallon but removes one coat, cures faster or reduces field touch-up often lowers the cost per unit. The HPC article What Are The Proper Methods for Touching Up High Performance Coatings? is a useful reference for planning field repairs of shop-applied systems.
Compliance: Air Rules and Shop Practicalities
Shop coating operations are stationary sources, so air permits and coating rules apply in addition to product selection. Depending on the facility, these can include the EPA area source rule for nine metal fabrication and finishing source categories (40 CFR Part 63, Subpart XXXXXX) and local rules such as the South Coast AQMD rule for coating of metal parts and products (Rule 1107).
VOC limits, transfer efficiency requirements and recordkeeping can all affect which products and spray equipment the shop may use. The facility's environmental staff should confirm requirements before a new system is approved. Other practical checks include:
- Equipment: Spray equipment compatibility and plural-component capability.
- Training: Operator familiarity with mixing, induction and application limits.
- Records: Quality control documentation that shows a customer what was applied and when.
Tnemec Options: Shop-Applied Primers and Finishes
Tnemec Series 1090 Endura-Shield is an aliphatic acrylic polyurethane finish. Tnemec Series 90-97 Tneme-Zinc is an aromatic urethane zinc-rich primer used where topcoats are applied the same day.
Tnemec Series 1071V Fluoronar is a low-VOC advanced thermoset solution fluoropolymer finish that Tnemec lists for OEM applications where long-term color and gloss retention is the priority.
Conclusion
The OEM coating decision works best in a fixed order: define the field exposure, choose the generic system that meets it with the fewest coats, and then tune cure, handling and preparation to the line. We recommend a short trial on production parts, with documented preparation and film build, before any new system goes into full production.
A coating that keeps the line moving is only a good choice if it keeps the equipment protected after it ships.
Field Verification Before Specifying
The following conditions are to be confirmed in the field with the applicable test before a system is finalized:
- Surface profile on production parts (ASTM D4417) against the primer requirement.
- Blast cleanliness against the specified SSPC/NACE standard, using SSPC-VIS 1 as a visual reference.
- Soluble salts on steel before coating where exposure to salts is possible (SSPC Guide 15 methods).
- Dry film thickness per coat and total, with attention to edges and welds (SSPC-PA 2 with ASTM D7091 gauges).
- Adhesion on production test panels (ASTM D4541 pull-off or ASTM D3359 tape method).
- Shop temperature, humidity and dew point during application and cure, against the product data sheet.
- Air permit and VOC/HAP rule requirements for the facility, confirmed by the facility's environmental staff.
We are happy to help. Contact a High Performance Coating Consultant in your region to review your shop conditions, end-use environment and coating specification.
Unveiling the Distinctions: USDA vs. FDA Coatings
Explore the critical differences between USDA and...
Understanding AAMA 2605 Standards for High...
AAMA 2605 is a stringent performance standard.